Quick Answer
A single pea-sized dot (3–4 mm diameter, ~0.3–0.5 mL) centered on the CPU IHS is correct for most desktop processors. Larger dies — HEDT, AMD Threadripper, Intel Xeon — require a thin crosshair or five-dot pattern. Spreading manually introduces air pockets. Excess paste migrates onto socket contacts and causes shorts.
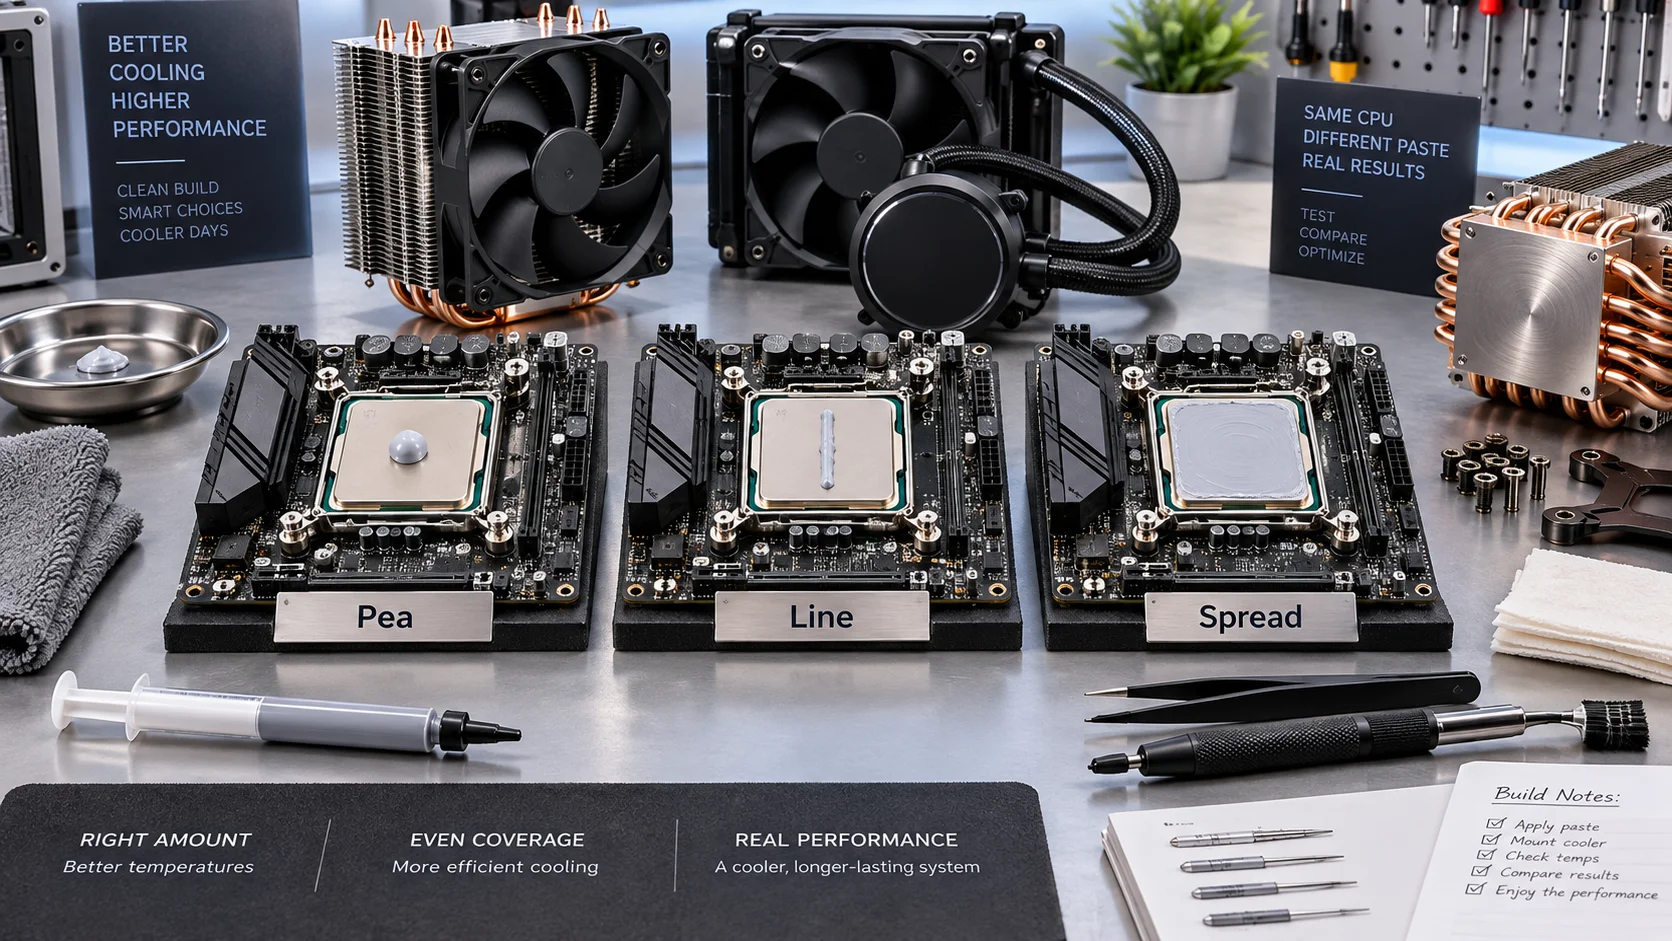
Applying thermal paste is the single most mechanically consequential step in a CPU cooler installation, yet it remains the most misunderstood. Too little paste leaves air gaps across the integrated heat spreader (IHS); too much risks capacitor fouling and socket contamination. The application pattern directly governs thermal resistance between silicon and heatsink, which determines sustained clock speeds, power limits, and long-term silicon degradation rates. This guide delivers exact volumes, validated patterns, and the engineering reasoning behind each — applicable to every consumer and prosumer platform available heading into 2026, from budget AM5 builds to flagship LGA1851 rigs.
The Physics of Thermal Interface Material (TIM) Application
Why Quantity Is a Precision Variable
Thermal paste — whether silicone-based, metal-oxide, carbon-loaded, or liquid metal — exists solely to fill microscopic surface irregularities between the CPU IHS and cooler base plate. Both surfaces appear flat to the naked eye but contain valleys up to 10 u00b5m deep under interferometric measurement. The paste fills those valleys; it does not conduct heat better than direct metal-to-metal contact. The ideal bond line thickness (BLT) after mounting pressure is applied sits between 50 u00b5m and 150 u00b5m. Below 50 u00b5m, dry spots emerge. Above 150 u00b5m, the excess TIM layer itself becomes a thermal resistor — paste conducts roughly 4–12 W/mu00b7K vs. copper’s 385 W/mu00b7K, so every unnecessary micron of paste thickness raises junction temperature.
Cooler Clamping Pressure and Spread Mechanics
Modern LGA and AM5 socket cooler mounts generate 40–80 N of clamping force. That pressure, distributed across the IHS surface area, spreads viscous paste radially outward. A standard 40 u00d7 40 mm desktop IHS combined with a pea dot of ~0.35 mL produces a spread diameter of approximately 38–42 mm under full clamping — virtually full coverage with zero overflow. Exceed ~0.6 mL on a standard IHS and paste will consistently reach and overflow the die edge. According to Intel Architecture Technical Documentation, contamination of LGA contact pads is a primary field return cause for motherboard RMA in consumer platforms.
Exact Volumes by CPU Platform and Die Size
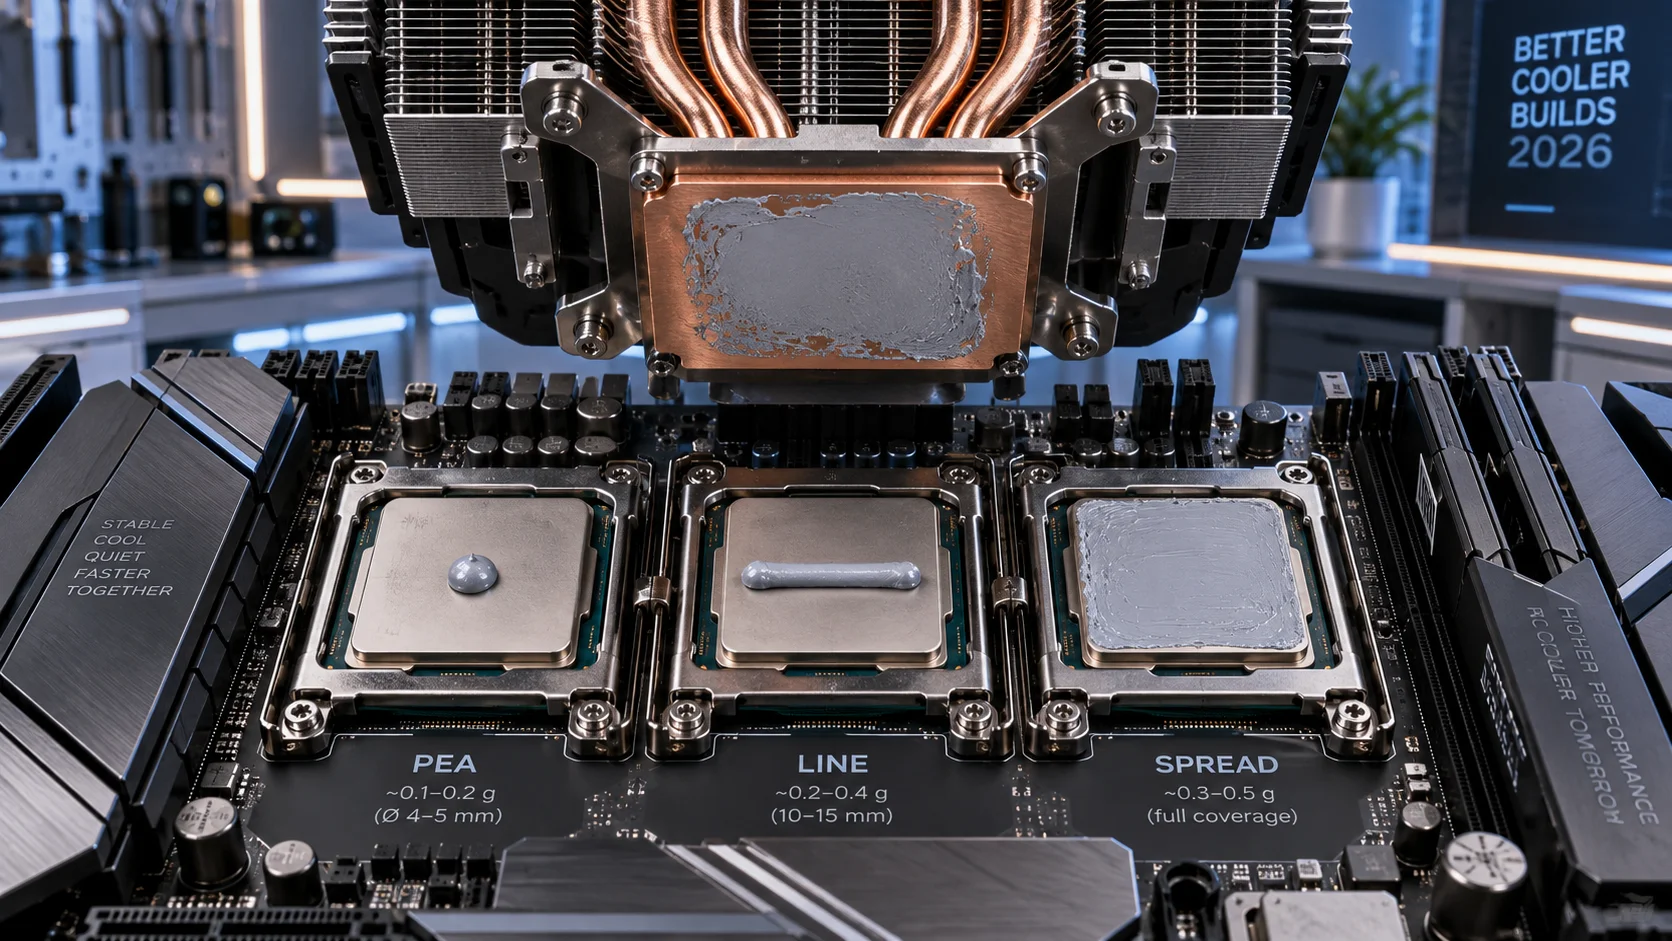
Standard Desktop CPUs (AM5, LGA1851, LGA1700)
The overwhelming majority of consumer CPUs — including AMD Ryzen 7000 and 9000 series and Intel Core Ultra 200 series — ship with a 37.5 u00d7 37.5 mm IHS. The pea-dot method (single centered dot, 3–4 mm diameter, 0.3–0.5 mL) is the industry-validated default. When you compare the thermal demands of platforms like the AMD Ryzen 5 9600X vs Intel Core Ultra 5 245K, both chips use the same pea-dot volume despite architectural differences — die topology and chiplet arrangement are sealed beneath the IHS and do not change surface application strategy for end users.
High-End Desktop (HEDT) and Workstation Platforms
AMD Threadripper 7000 (sTR5 socket) and Intel Xeon W processors use IHS dimensions of 68 u00d7 51 mm or larger. A single pea dot will not cover this surface under mounting pressure. Validated patterns for HEDT are the five-dot (X) pattern or a thin crosshair line — both deposit approximately 1.0–1.5 mL total. The objective is identical: achieve u226595% IHS coverage at the target BLT after clamping. Under-coverage on a 12-chiplet Threadripper package results in thermal differentials between CCDs exceeding 8°C, which the scheduler interprets as a throttle trigger.
Laptop and Mobile CPUs
Laptop thermal modules are pre-applied at the factory with phase-change pads or low-viscosity TIM on bare dies (lidless packages). Repasting a laptop die requires a micro-dot of 0.1–0.15 mL centered precisely on the exposed silicon, as die area may be as small as 150 mmu00b2. Overflow onto PCB components in an ultrabook chassis is irreversible without full board replacement.
Pattern Comparison: Pea, Line, X-Dot, Spread
| Pattern | Volume (mL) | Best Platform | Coverage Efficiency | Air Pocket Risk | Overflow Risk |
|---|---|---|---|---|---|
| Pea Dot (single center) | 0.30–0.50 | All standard desktop (AM5, LGA1851, LGA1700) | 95–99% | Very Low | Low |
| Thin Line (horizontal) | 0.35–0.55 | Rectangular IHS (some LGA2066) | 92–97% | Low | Low–Medium |
| X-Dot / Five-Dot | 1.00–1.50 | HEDT: Threadripper, Xeon W | 96–99% | Very Low | Low (if dosed correctly) |
| Crosshair Line | 0.80–1.20 | HEDT, large IHS workstation chips | 93–98% | Low | Medium |
| Manual Spread (spatula) | 0.40–0.70 | Any — but not recommended | 85–94% | High | Medium–High |
| Micro-Dot (laptop/bare die) | 0.10–0.15 | Mobile CPUs, lidless dies | 90–97% | Low–Medium | High if exceeded |
Why Manual Spreading Underperforms
Pre-spreading paste with a spatula or card before cooler installation introduces laminar air inclusions at the TIM surface during the spreading stroke. These micro-bubbles — invisible at 1 mm scale — become insulating voids once the cooler seats. Thermal imaging of manually spread applications vs. pea-dot applications consistently shows 1–3°C higher peak hotspot temperatures on the manually spread samples under sustained AVX-512 loads. The pea dot, pressed by cooler clamping force, expels air radially and achieves a denser, void-free bond line.
Paste Selection: How TIM Type Affects Quantity Guidance
Viscosity and Spread Radius
High-viscosity pastes (e.g., Thermal Grizzly Kryonaut: ~130 Pau00b7s, Noctua NT-H2: ~90 Pau00b7s) spread less under identical clamping force than low-viscosity compounds (e.g., Arctic MX-6: ~40 Pau00b7s). For high-viscosity pastes, size the pea dot toward the upper bound — 4 mm diameter rather than 3 mm — to guarantee full IHS coverage. For low-viscosity pastes, err toward the lower bound (3 mm) to prevent overflow, particularly on LGA1851 boards where contact pads sit 2–3 mm from the IHS edge. Builders pairing their TIM choice with premium Z890 platforms — detailed in the ASUS ROG Maximus Z890 Hero vs MSI MEG Z890 ACE comparison — should note that both boards use tightly toleranced LGA1851 retention frames with minimal clearance for paste overflow.
Liquid Metal: Special Rules Apply
Liquid metal compounds (Thermal Grizzly Conductonaut, Coollaboratory Liquid Ultra) carry 73 W/mu00b7K conductivity — roughly 10u00d7 standard silicone paste. However, liquid metal is electrically conductive and will short SMD components on contact. Application volume must not exceed 0.05–0.08 mL per application point, dispensed via the included needle applicator in a micro-dot pattern. Liquid metal must never contact aluminum cooler surfaces — it amalgamates with aluminum and destroys the heatsink base within hours. Confirmed compatible cooler materials: copper, nickel-plated copper, stainless steel.
Phase-Change Pads and Pre-Applied Compounds
Many retail CPU coolers — including stock AMD Wraith Prism and Intel Laminar coolers — ship with a pre-applied phase-change pad on the contact plate. Do not add additional paste on top of a factory pad. The pad transitions to liquid state at 50–60°C and self-spreads. Adding TIM over a pad produces a double layer with a combined BLT exceeding 300 u00b5m — measurably worse than either material alone.
Step-by-Step Application Protocol for Standard Desktop CPUs
- Clean both surfaces. Apply isopropyl alcohol (u226590% concentration) to a lint-free cloth. Wipe the IHS center in a single direction, then rotate 90° and repeat. Clean the cooler contact plate identically. Allow 60 seconds for complete evaporation before proceeding.
- Dispense the pea dot. Hold the syringe vertically over the IHS center. Apply steady pressure until a 3–4 mm dome forms — roughly the size of a split pea. Stop. Do not spread.
- Seat the cooler without rotation. Lower the cooler straight down onto the CPU. Do not rotate or twist during initial contact — rotation smears paste asymmetrically. Begin tightening retention screws in a diagonal (X) sequence, one quarter turn per pass, to equalize clamping pressure.
- Verify torque completion. Most consumer cooler mounting hardware bottoms out at 3–5 Nu00b7m. Resistance should feel firm and uniform across all four mounting points. Uneven resistance indicates a warped cooler base or misaligned standoffs — remove, inspect, and re-apply.
- Log baseline thermals. Boot to OS and run a 10-minute full-load stress test (Prime95 small FFTs or AIDA64 FPU). Record peak Tdie/Tjunction. For 65W-class CPUs, peak under full load should remain below 85°C. For 125W–253W class CPUs, sustained temperatures should stay below 95°C Tjunction before thermal throttle engages.
Builders selecting CPUs for gaming rigs should cross-reference our desktop CPU benchmarks & reviews to align TIM selection and application method with the specific TDP and cooler pairing for their target chip. Similarly, GPU thermal paste repasting — relevant for anyone maintaining an aging graphics card — follows parallel principles covered in our graphics card tests & GPU guides. Performance decisions around GPU tier — including high-bandwidth configurations like the Radeon RX 9060 XT 8GB vs 16GB comparison — are equally sensitive to long-term thermal management quality.
Diagnostic Symptom Matrix: Identifying Bad TIM Application
Thermal Signatures of Common Errors
| Symptom | Likely TIM Cause | Measured Delta vs. Correct | Corrective Action |
|---|---|---|---|
| Idle temps 15–20°C above ambient | Insufficient paste — dry spots on IHS | +10–18°C Tdie | Remove, clean, re-apply full pea dot |
| Temps spike then throttle within 30 s of load | Air void at die center — paste ring with hollow core | +12–22°C Tdie | Remove, inspect spread pattern, re-apply |
| Asymmetric core temp spread (>8°C core delta) | Off-center dot or uneven cooler seating | +6–14°C hottest core | Check mounting torque sequence, re-center application |
| POST failure / no boot after cooler install | Paste overflow onto LGA contact pads | N/A — electrical fault | Remove CPU, inspect socket, clean pins with IPA |
| Gradual 5–8°C temp rise over 12–18 months | TIM dry-out / oil separation (silicone-based paste) | +5–8°C Tdie | Annual repaste cycle; switch to higher-grade compound |
| System stable, temps within spec but slightly high | Excess paste — BLT too thick, paste acting as insulator | +2–5°C Tdie | Remove, apply smaller dot, verify BLT after seating |
Final Diagnostic Verdict & Maintenance Checklist
Thermal paste application is not a matter of aesthetic preference — it is a precision materials engineering step with direct measurable impact on CPU junction temperature, power delivery headroom, and silicon longevity. Overclocked or power-limited builds operating near their thermal ceiling lose 50–200 MHz of sustained all-core boost for every 5°C of avoidable TIM-induced temperature rise. The guidance below is the minimum viable maintenance standard for any build going into 2026.
- Standard desktop (AM5, LGA1851, LGA1700): Single pea dot, 3–4 mm, 0.30–0.50 mL, centered on IHS. Do not spread manually.
- HEDT / workstation (sTR5, W790): Five-dot X pattern or thin crosshair, 1.0–1.5 mL total, distributed across IHS thirds.
- Laptops / lidless mobile: Micro-dot, 0.10–0.15 mL, maximum precision — any overflow risks permanent PCB damage.
- Liquid metal: 0.05–0.08 mL per site, copper/nickel coolers only, mask all surrounding SMD components with kapton tape before application.
- Annual maintenance: Repaste every 12–18 months with silicone-based compounds; every 24–36 months with premium ceramic or carbon compounds (slower dry-out rate).
- Post-install verification: Run a 10-minute full-load test within 30 minutes of installation. Log baseline temperatures for future comparison. Any reading >10°C above expected Tjunction at stated TDP warrants immediate removal and inspection.
- IPA concentration: Use u226590% isopropyl for both pre-application cleaning and paste removal. Lower concentrations leave water-based residue that degrades adhesion on re-installation.
- Cooler removal interval: Remove and inspect the TIM bond line whenever peak thermals climb more than 7°C above the original post-install baseline — this threshold reliably indicates compound failure before thermal throttle becomes routine.